Hotline: 098 712 3398 Email: [email protected]
20 SKUs

Round dies

Showing 1-3 19 views

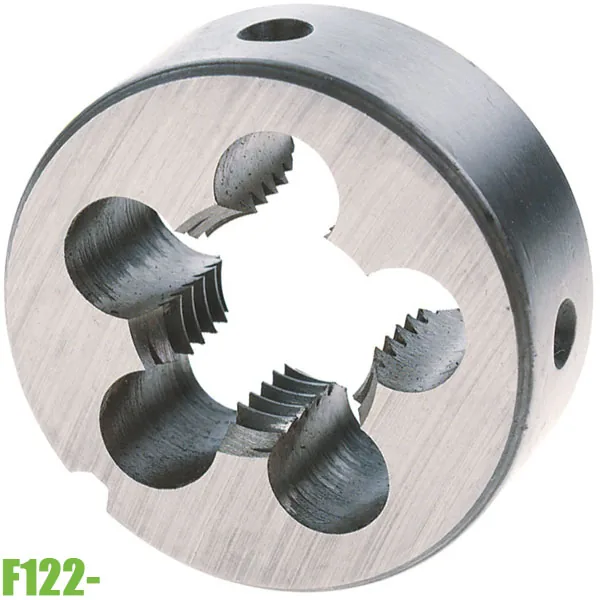
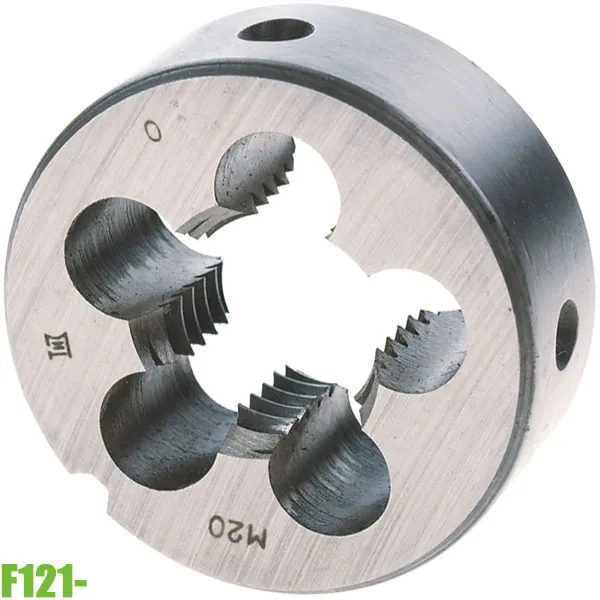
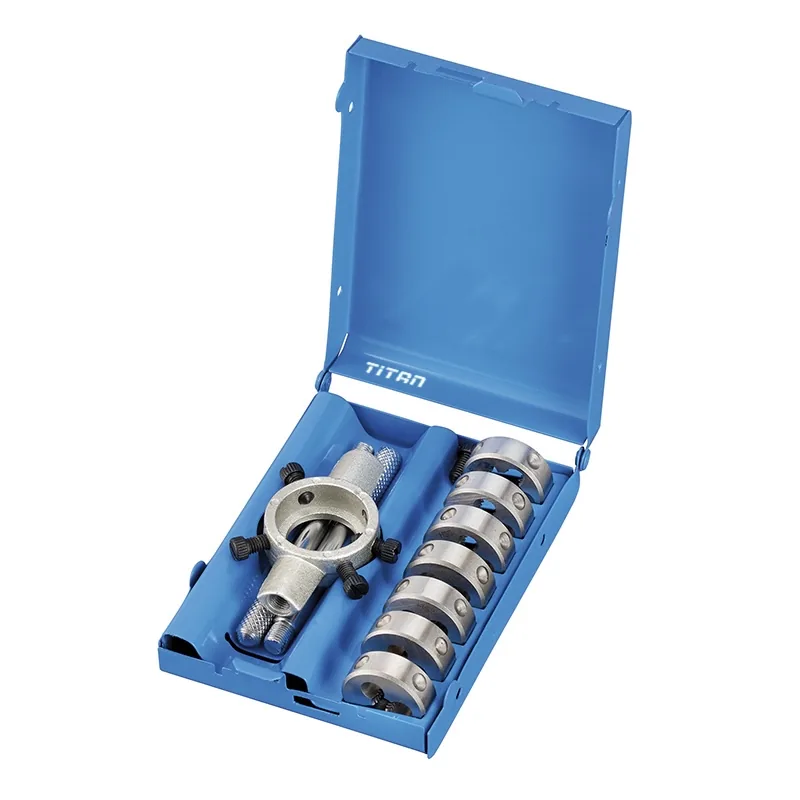
Round dies serve to create external threads on shafts, pipes and metal parts in machining. The metric round dies and inch round dies product group from FERVI is manufactured from HSS steel, compliant with DIN 223 standard for metric threads and DIN 5158/B for gas threads. The metric range covers sizes from M3 to M12 with coarse pitch, while the inch range meets gas thread pipe requirements according to British standard. The F121 line provides individual external thread round dies, the F122 line serves gas threads, and the F123 set integrates 7 round dies from M3 to M12 with holder. Products are imported directly from Italy, ensuring accuracy of flute angle and thread pitch, suitable for machine shops, equipment maintenance and industrial assembly.
Drag product cards to reorder this category. Release to save immediately.

Round dies serve to create external threads on shafts, pipes and metal parts in mechanical machining. The metric round die and inch round die product range from FERVI is manufactured from HSS high-speed steel, complying with DIN 223 standard for metric threads and DIN 5158/B for gas threads. The metric system covers sizes from M3 to M12 with coarse pitch threads, while the inch system meets gas thread requirements according to British standards. The F121- line provides single external threading dies, the F122- line serves gas threads, and the F123 set integrates 7 round dies from M3 to M12 with a holder. Products are officially imported from Italy, ensuring accuracy of thread angle and pitch, suitable for mechanical workshops, equipment maintenance and industrial assembly.

Round dies play an important role in mechanical machining, serving to create external threads on shafts, pipes or metal parts requiring assembly. This tool helps workers create spiral grooves according to technical standards, ensuring precise connection with nuts or corresponding internal threaded parts. In production and maintenance practice, round dies appear in many forms to meet different thread systems.

The metric system uses thread pitch measured in millimeters, common in European and Vietnamese industry. The inch system applies thread pitch calculated by the number of grooves per inch, often found in American imported equipment or gas pipes. Each thread system requires a separate round die to ensure accuracy of groove angle, thread pitch and nominal diameter. Manufacturing material directly affects service life and machining capability.

HSS high-speed steel withstands heat well, maintains sharp edges long when cutting ordinary carbon steel. Some premium lines are coated with TiN or TiAlN to increase surface hardness and reduce friction. When selecting round dies, users need to clearly identify the thread system, nominal diameter, thread pitch and type of machining material. Using the correct size avoids thread damage, reduces excess cutting force and extends tool life.

Lubrication with cutting oil or machine oil during threading helps dissipate heat, reduce wear and improve the smoothness of thread grooves.
Classification by thread system

The thread system determines the spiral groove structure, thread pitch and profile angle of round dies. Each system follows separate standards and cannot be interchanged in assembly. Understanding the characteristics of each system helps select the right tool for each type of part.

Metric round dies create threads according to ISO standards, designated M with nominal diameter. Standard thread pitch is called coarse pitch, suitable for general assembly. Fine pitch threads are used when high precision is required or space is limited. The F121- line uses HSS high-speed steel, complying with DIN 223 for metric coarse pitch threads. This material withstands heat well, maintains sharp edges when machining carbon steel and light alloys. The F123 set includes seven round dies from M3 to M12, accompanied by a round holder measuring twenty-five by nine millimeters. This set serves multi-size threading needs in small mechanical workshops or field maintenance.

Inch round dies apply to gas pipes, water pipes and British-American standard equipment. Thread pitch is calculated by the number of grooves per inch, designated TPI. The F122- line complies with DIN 5158/B, belonging to the gas thread die category. This type creates tapered or parallel threads on steel pipes and copper pipes used in pneumatic and water systems. Profile angle and thread pitch differ from the metric system, ensuring gas-tight connection with nuts or corresponding pipe fittings. Imported from Italy, the F122 line meets high precision requirements in industrial piping installation.

Material and durability

Manufacturing material determines heat resistance, hardness and service life of round dies. HSS high-speed steel is a popular choice thanks to the balance between cost and performance. This alloy contains tungsten, molybdenum and chromium, maintaining hardness at high temperatures during continuous cutting.

The F121- line uses premium HSS high-speed steel, withstanding force well when creating threads on medium-hardness carbon steel. Fine grain structure helps sharp cutting edges, reducing force needed when rotating the round die. High durability allows machining many parts before needing regrinding or replacement. Some premium lines are coated with yellow TiN or purple TiAlN, increasing surface hardness to sixty-five to seventy HRC. This coating reduces friction, dissipates heat quickly and extends service life double compared to uncoated HSS. When machining hard materials such as alloy steel or stainless steel, the coating helps reduce wear and prevent chip adhesion.

Sizes and collections

Round die size must match precisely with the nominal diameter and thread pitch of the part to be machined. Small deviations cause loose or overly tight threads, affecting connection durability. Multi-size collections help small workshops remain flexible without buying individual pieces separately.

The F123 set contains seven round dies from M3 to M12, covering the common size range in electronics assembly, precision mechanics and equipment maintenance. The round holder measuring twenty-five by nine millimeters keeps the round dies organized, easy to identify sizes when needed. This set saves storage space and reduces tool search time. The F121- line provides individual sizes separately, suitable when only needing to supplement a specific diameter or replace a damaged round die. Users should check standard or fine thread pitch before ordering, avoiding confusion causing waste.

Applications in machining

Round dies serve to create external threads on shafts, bolts, pipes and parts requiring assembly with nuts or fittings with internal threads. This tool appears in mass production, equipment maintenance and field repair. Thread accuracy directly affects durability and load-bearing capacity of connections.

In mechanical production, metric round dies create threads on motor shafts, structural bolts and machine parts. The F121- line with metric coarse pitch threads meets standard assembly requirements, easy to disassemble during maintenance. Inch round dies such as F122- serve gas pipe and water pipe installation in industrial systems. Gas thread tapered threads create gas-tight connections thanks to slight slope, suitable for medium pressure. In maintenance, the F123 set helps repairmen quickly fix damaged thread bolts or create new threads on re-machined shafts. Seven sizes from M3 to M12 cover most needs in small workshops and mobile maintenance stations.
Usage notes

Using proper technique extends round die service life and ensures thread quality. Prepare hole or shaft diameter to correct standards before threading. Oversized diameter causes shallow threads, undersized increases cutting force and easily breaks round dies. Applying cutting oil or machine oil to the machining surface helps dissipate heat, reduce friction and improve thread groove smoothness.
Rotate the round die slowly, avoiding excessive force causing cutting edge breakage. After each forward rotation, reverse half a turn to break chips and reduce pressure. Check perpendicularity between round die and machining shaft, avoiding misaligned threads causing difficult assembly. After use, clean chips and adhered oil, store in a dry place to avoid rust. Regrind cutting edges when threads are no longer sharp or chipping appears. Use fine grinding stones, maintain standard profile angle so the round die continues to operate accurately.
This product range provides external threading solutions for multiple standard systems and sizes. Selecting the correct thread system, material and size helps optimize machining performance and reduce tool maintenance costs.